

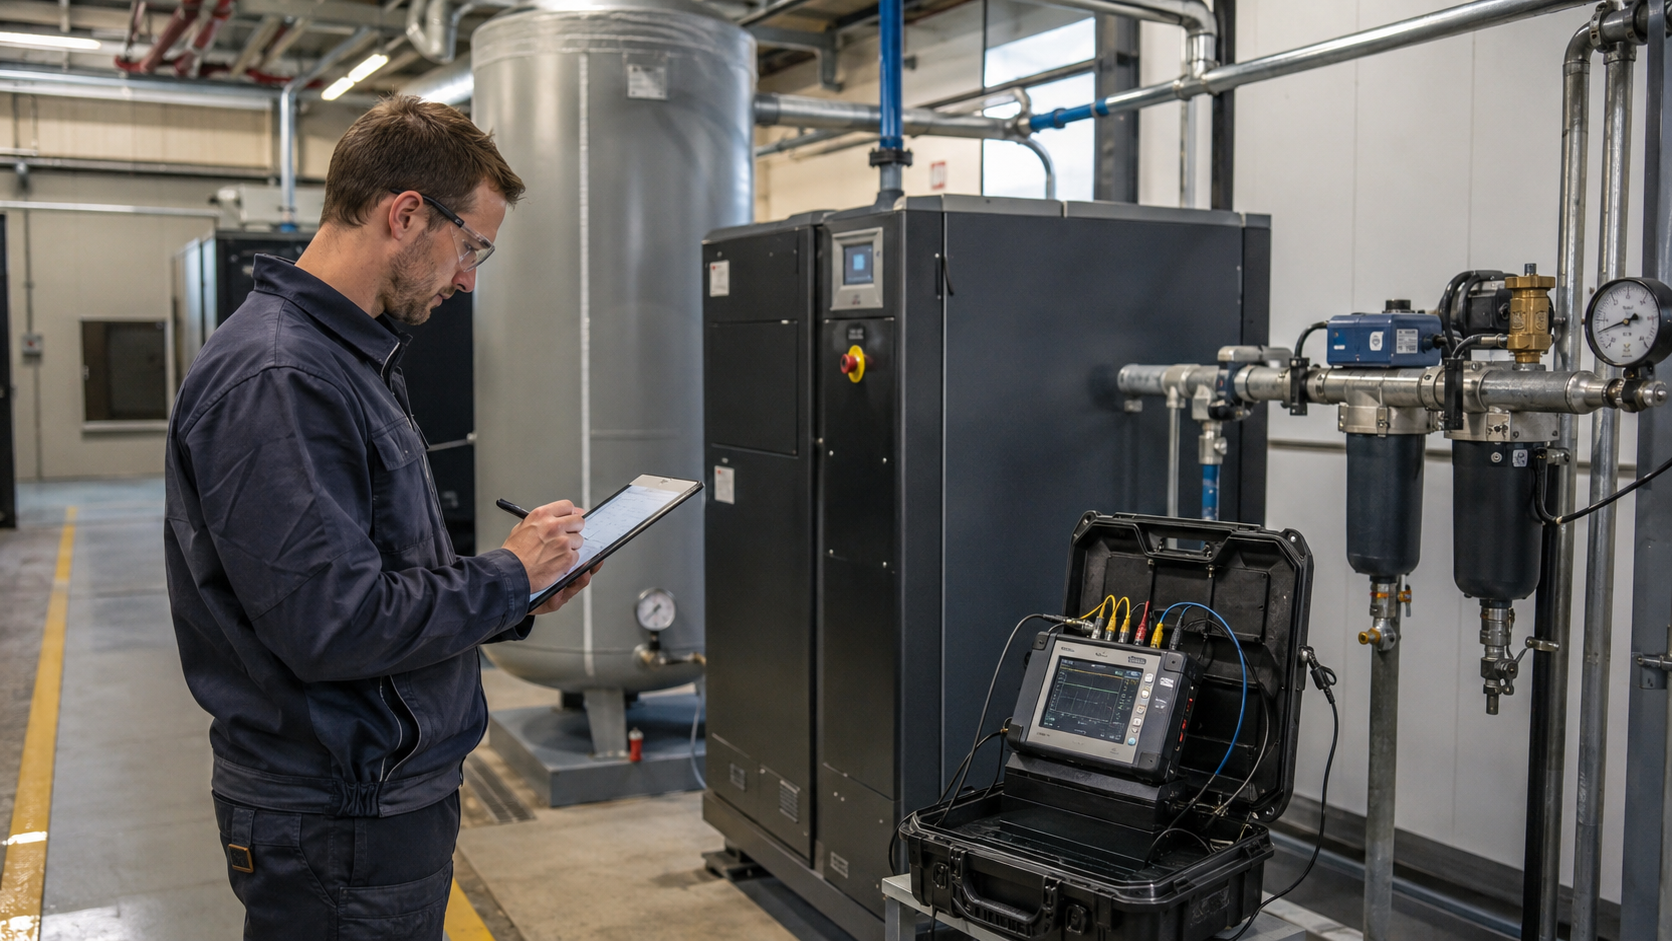
A compressed air audit is useful only if it reconstructs how the entire system actually operates. A pressure reading at the compressor, a check of nameplates or a one-off leak survey is not enough to determine whether the system is operating efficiently or where the real problem lies.
A reliable assessment requires several data sets to be considered together: electricity consumption, the amount of compressed air produced and used, pressure at different points in the system, compressor operating states, end-use requirements and — where the process requires it — compressed air quality. These data also need to be correlated with what was happening in production at the same time.
In practice, the most important question is not “what parameter to measure?” but “what measurements to take simultaneously, at which locations, and for how long, to draw unambiguous conclusions?”
What should a compressed air audit actually provide?
A technical audit should provide answers to at least four questions:
- How much electricity does the system consume, and under what operating conditions does this consumption occur?
- How much compressed air is generated, and where do the largest or most variable demands occur?
- Are the required pressure and air quality ensured at the point of use without unnecessarily raising the parameters of the entire system?
- Does the observed problem mainly arise from compressed air generation, transmission, or the way the air is used at the end uses?
This approach is consistent with ISO 11011:2013, which treats a compressed air system as three interconnected functional subsystems: supply, transmission and demand. The standard does not limit the assessment to the compressor room — it covers the entire chain from energy input to the work performed by end-use equipment.
As of August 21, 2026, ISO 11011:2013 remains the published edition. ISO has started work on Edition 2, but project ISO/AWI 11011 is only in the preparatory stage and has not yet replaced the current published edition.
1. First, define the audit boundaries and a representative operating cycle
Before selecting measurement instruments, define which part of the system will be assessed. Measurements are planned differently for a single compressor room with one header than for a plant with several compressor rooms, a ring main, local boosters and end uses that require different pressure levels.
The audit boundary should define, among other things:
- which compressors and auxiliary equipment are included in the energy balance;
- whether flow measurement covers the entire compressor room, selected main lines, or individual end uses as well;
- where the analyzed network section begins and ends;
- which end uses are critical to production;
- what production states should be considered normal, peak, and non-production.
Equally important is establishing a representative cycle. If the plant produces in a similar manner around the clock, one full cycle covering all characteristic states may be sufficient. If products, number of lines, number of shifts, weekend work, or production campaigns change, the recording must capture these differences.
There is no single correct number of hours or days for every plant. The measurement period is appropriate when it captures all operating states that materially affect flow, pressure and power demand.
Auditor’s comment: a short spot measurement can confirm a specific problem, but it is rarely sufficient to describe a system with variable demand. If the second compressor only turns on a few times per shift, and the measurement was taken outside these events, the most important part of the profile simply won’t be included in the data.
2. What documents and data to collect before the site visit?
A good site visit begins before entering the compressor room. The more data that can be collected beforehand, the easier it is to plan appropriate measurement points and avoid a situation where, after several days of recording, it turns out that information needed to interpret the graph is missing.
Before the visit, it is worth collecting:
- the compressed air system diagram, if available, or at least a plant layout with the routing of main lines;
- a list of compressors, dryers, air receivers and the main air-treatment components;
- compressor datasheets, manufacturer’s performance data, and information on the pressure for which parameters are given;
- data on compressor control methods: load/unload, start/stop, modulation, VSD/VFD, master controller;
- readings of operating hour meters and operating state history;
- data from local energy meters, SCADA, BMS, or monitoring systems, if available;
- pressure history, alarms, shutdowns, and service records;
- production and shift schedule;
- information on the number of active lines, product changes, campaigns, and planned shutdowns;
- required pressure and air quality for key end uses;
- history of filter replacements, dryer service, and condensate problems;
- previous leak detection reports with repair status.
Manufacturer’s data is useful but does not replace measurements. The compressor performance parameter may be given for specific reference conditions and pressure. If it is compared with an in-system measurement, it is first necessary to check whether the compared values have the same definition.
3. System inventory – what needs to be recorded on-site?
The inventory should not end with the number of compressors. The entire air flow path and the points where its parameters change must be reconstructed.
| Element | What to record | Why it matters |
|---|---|---|
| Compressors | type, model, drive power, declared capacity, set pressures, control type, hour meters, role in sequence | allows correlating power consumption with capacity and control method |
| Dryers | type, capacity, control method, energy consumption or regeneration air usage, dew point, alarms | drying can generate both energy consumption and air losses, as well as pressure drops |
| Filters and separators | type, location, nominal flow, differential pressure indicators, service status | a dirty or improperly selected component can restrict flow |
| Air receivers | capacity, operating pressure, location, connection method to the network | affect system dynamics and ability to handle short peaks |
| Network | diameters, material, lengths, branches, loops, constrictions, valves, inter-hall connections | allows interpreting pressure drops and local restrictions |
| End uses | required pressure, quality, consumption characteristics, duty cycle, local reducers and filters | shows what parameters are actually needed by the process |
Changes made after the original design are particularly important: an added production hall, a new line, an additional filter, a long flexible hose, a temporary supply or an end use connected to an undersized branch. Such elements may simply not appear on a drawing from several years ago.
4. Operating hour, load, and idle hour meters
Reading compressor meters is a good starting point, but only if it is known exactly what each value means in a given controller.
In a compressor operating in load/unload mode, it is worth distinguishing at least:
- total run time;
- time under load;
- time operating unloaded;
- standby or ready time;
- number of starts, if the controller records it.
In a variable-speed compressor, operating hours alone say much less. A load or speed distribution is needed, and ideally a simultaneous power and flow profile.
A high proportion of idle time may indicate a control problem or a mismatch between compressor configuration and demand, but energy losses cannot be calculated from idle time alone. For that, actual power consumption in that state is needed.
For a simplified balance, the following relationship can be used:
energy over period = sum of power in individual states × duration of these states.
So, if a compressor is loaded for part of the time, unloaded for part of the time, and stopped for part of the time, each of these states must be treated separately. With several compressors, it is also necessary to check whether their states overlap and how the sequencing works.
5. Electricity measurements – what to measure and where?
The basic quantity is the actual active power consumed by the compressor or the entire compressor package, and the energy consumed during the analyzed period.
If the goal is to evaluate a specific compressor, the measurement should allow seeing:
- power during full load;
- power during unloaded operation;
- power at partial load;
- power changes with VSD compressor speed changes;
- starts, stops, and standby periods.
It is best to record kW and kWh directly. Current measurement alone can be diagnostically useful, but with a variable power factor and changing operating conditions, it should not automatically replace active power measurement.
The measurement boundary must also be defined. In one plant, “compressor room energy” means only compressors, while in another, it also includes dryers, fans, pumps, cooling systems, and auxiliary equipment. Without recording this boundary, two kWh results may not be comparable.
A practical solution is to synchronize the energy logger with flow, pressure, and controller state recording. Then, it is possible to check not only how much energy the compressor consumed, but also what the system actually delivered at the same time.
Temperature as a supplementary measurement
Temperature is not an independent indicator of overall system efficiency, but in specific diagnostic tasks, it is needed for correct interpretation of results. It is worth recording, among other times, when assessing suction conditions, cooler operation, air temperature before the dryer, or the cause of dew point changes. When building a baseline, U.S. DOE lists temperature alongside power, pressure, and flow as one of the quantities measured under various operating conditions. The range of temperature points should result from the audit’s objective, not from the assumption that every point in the system must always be measured.
6. Measurement and recording of compressed air flow
Without flow information, it is difficult to assess whether high power consumption results from high actual demand or inefficient compressor operation.
The most important point is usually the main line exiting the compressor room. In a more complex system, additional measurements may be needed:
- on main lines supplying individual halls;
- on branches with high or unstable consumption;
- upstream of an end use that causes demand spikes;
- in the part of the system suspected of high non-production consumption.
When choosing the measurement location and method, it is necessary to check the flowmeter’s measuring range, manufacturer’s installation requirements, possible influence of flow disturbances, air quality, and the conditions to which the result is converted.
Particular caution is required when comparing units. A result in m³/h under operating conditions is not automatically equivalent to Nm³/h or flow referenced to other conditions. The report must state the reference conditions and apply them consistently.
The same applies to comparing measurements with the compressor’s catalog capacity. ISO 1217:2009 specifies acceptance test methods for, among other things, the volume flow rate and power consumption of displacement compressors. If manufacturer data based on this standard is used, it is still necessary to compare the pressure and conditions for which the declared value was given with the actual operating point.
From the flow profile, it is worth determining not only the average, but also the baseline level, peaks, minimum and maximum demand, duration of characteristic states, and the volume of air consumed in a given period.
7. Pressure measurements – one pressure gauge is not enough
The pressure at the compressor indicates the conditions in the compressor room. It does not yet indicate the pressure reaching the machine at the end of the hall.
Therefore, when analyzing pressure problems, it is advisable to place loggers at several points, for example:
- on the compressor room manifold;
- before and after the main treatment system, if we want to assess its impact;
- at the beginning and end of the main line;
- in a remote or problematic part of the plant;
- directly upstream of a critical end use;
- before and after a local filter, reducer, valve, or line, if a restriction is suspected.
Simultaneous measurement provides the greatest value. If the pressure in the compressor room was measured in the morning and at the end of the hall in the afternoon, it is unknown whether the difference results from the network or simply from different demand.
All values should have a clearly defined basis – for example, bar(g) for gauge pressure. Mixing gauge and absolute pressure in calculations is a simple way to generate erroneous conclusions.
8. How to analyze pressure drops?
Pressure drop must be analyzed as the difference between two points at the same time and under a known system load.
If:
- pressure in the compressor room remains stable;
- flow increases;
- and pressure in a remote part of the system drops sharply,
then the problem may be in transmission: too small a diameter, a constriction, filter, valve, flexible hose, or another element with increasing resistance.
If the pressure drop occurs simultaneously in the compressor room and throughout the network, check the balance between instantaneous demand and available capacity, compressor sequencing, buffering, and events on the demand side.
It is not advisable to adopt one universal “acceptable pressure drop” for every system. The criterion should result from the minimum pressure required by the process, the characteristics of specific components, and the flow conditions under which the measurement was taken.
A common mistake is to raise the pressure of the entire compressor system simply because one end use at the far end of the plant receives insufficient pressure. If the cause is a local restriction, increasing compressor pressure may only mask the problem.
9. Compressed air quality and dew point – only in relation to the process
Not every system requires the same air quality. Therefore, an audit should start by asking what the process actually needs, and only then assess drying and filtration.
ISO 8573-1:2010 classifies compressed air purity in relation to particles, water, and oil. The standard also indicates other types of contaminants, but this does not mean that a full set of laboratory tests must be performed in every audit.
If humidity is critical for the process, one of the important parameters is the pressure dew point. Measurement must be performed and reported considering sample collection conditions, pressure, and indication stabilization. ISO 8573-3:1999 describes humidity measurement methods, sampling principles, uncertainty assessment, and reporting; the standard is still published, although it is currently under review.
In practice, therefore, it is not the “lowest possible dew point” that is analyzed, but the dew point required by the given process and how the dryer maintains this parameter under variable load.
Similarly with filtration: more precise filtration is not automatically better if the process does not need it, and additional elements increase pressure drop or require more frequent maintenance.
10. Leak detection is part of the audit, not the entire audit
Leaks are an important source of unproductive compressed air consumption, but an ultrasonic survey alone will not answer whether compressors are operating within the correct range, whether control is well configured, or whether the network has sufficient capacity.
As part of a full audit, leak detection may include:
- localization and marking of leaks;
- assignment of location and equipment;
- assessment of repair priority;
- re-verification after fault removal;
- estimation of flow lost to leaks, if the method and data used allow for reliable quantification.
The decibel value from a detector alone should not be converted to annual kWh without additional basis. For energy assessment, a method linking the leak to flow, pressure, occurrence time, and the characteristics of the generation system is needed.
Flow measurement during a production shutdown can also be very useful, provided it is known which end uses must remain in operation. This makes it possible to estimate total non-production demand rather than only the sum of detected leak points.
Detailed leak detection is a separate measurement task. In a full audit, its results should be included in the common balance of flow, operating time, and energy, instead of functioning as a standalone “audit result”.
11. End-use demand analysis
If the audit ends at the compressor room, it is easy to overlook the cause located on the other side of the system.
For the most important end uses, determine:
- minimum required pressure at the device inlet;
- instantaneous and average air consumption;
- duty cycle;
- required air quality;
- presence of local filters, reducers, and valves;
- length and diameter of connection lines;
- whether the end use operates continuously or only in short pulses;
- whether consumption is directly related to production.
Pulsed end uses require particular attention. A machine may draw a very high flow for a few seconds even though its average consumption is low. This type of demand can cause short pressure drops and start an additional compressor, effects that disappear in hourly averaged data.
It is also worth distinguishing production demand from consumption that does not perform useful work: constant purges, poorly adjusted nozzles, open lines, unnecessary supply to idle equipment, or applications for which another medium source could be considered. The audit itself should primarily identify and measure such cases; the detailed sequence of modernizing the entire system belongs to optimization analysis.
12. How to link compressed air measurements with plant production?
Energy profiles without production data are easily misinterpreted. A decrease in energy consumption may result from improved efficiency, but equally well from lower production.
Therefore, all loggers should have synchronized time, and the measurement data should be supplemented with:
- operation or shutdown of individual lines;
- number of shifts;
- type of product manufactured;
- number of pieces, tons, or other appropriate production measure;
- changeovers, cleanings, startups, and shutdowns;
- events causing atypical air consumption.
Only then can it be assessed why compressed air consumption was different on two seemingly similar days.
Specific power – a useful indicator, but only under clearly defined conditions
A useful metric for assessing a compressor or compressor group is specific power: the ratio of power input to delivered air flow. U.S. DOE uses the term specific power for this metric.
For example, under the same flow reference conditions and comparable pressure:
- system A consumes 70 kW and delivers 10 m³/min – specific power is 7 kW/(m³/min);
- system B consumes 60 kW and delivers 7.5 m³/min – specific power is 8 kW/(m³/min).
Thus, the lower power of system B alone does not mean better operation. It delivers less air in relation to the power consumed.
However, this indicator should not be compared without checking:
- discharge pressure;
- flow reference conditions;
- measurement boundary;
- load condition;
- configuration of operating compressors.
For the entire plant, it is also useful to compare system energy with production, for example, kWh per ton of product or kWh per 1000 pieces. This is an indicator of the process’s energy intensity, not a standalone measure of compressor efficiency. If the product range or technology changes, this must be taken into account when comparing.
13. Why can a short spot measurement lead to erroneous conclusions?
Assume that at 10:00 the plant is using 600 m³/h, one compressor is running, pressure is stable and no problem is visible. At 11:20, a high-flow pulsed end use starts, pressure at the far end of the plant drops and the controller starts a second compressor. At 12:00, the system returns to its initial state.
A measurement taken only at 10:00 will not record the event that may have the greatest impact on system operation.
Recording is particularly needed when:
- demand changes between shifts;
- production is campaign-based or batch-based;
- some machines operate only periodically;
- several compressors are controlled sequentially;
- short pressure drops occur;
- dryers or auxiliary equipment operate cyclically;
- significant non-production consumption occurs;
- the plant has different profiles on weekdays and weekends.
The recording frequency must also be chosen to match the phenomenon. If the problem lasts a few seconds, hourly recording is useless. If analyzing a monthly trend, very fast sampling may be unnecessary. What matters is the ability to capture the events we want to explain.
14. How to distinguish a compressed air generation problem from a distribution-system or end-use problem
The most valuable part of the audit begins when measurements are analyzed together.
| What is visible in the data | Probable problem area | What to check next |
|---|---|---|
| high power at low flow, and network pressure is stable | generation / compressor control | idle running, modulation, sequence, operating point, and actual power consumption |
| compressor room pressure stable, but at the end of the network it drops during flow increase | transmission | filters, diameters, valves, constrictions, main lines, and local connections |
| pressure drops simultaneously throughout the system, and a large flow spike appears at the same time | supply and demand balance | production event, available capacity, buffering, control |
| compressors cycle even when production is stopped, and flow does not drop to a low level | unproductive demand | leaks, automatic drains, end uses left pressurized |
| main line has correct pressure, but a single machine does not | local end use / connection | reducer, filter, valve, line, quick couplings, and local peak |
| dew point deteriorates at a specific load | treatment or measurement conditions | dryer capacity, regeneration, flow, pressure, sample collection point |
The table does not replace diagnosis. Each of these signals primarily indicates where to direct the next step of analysis.
Auditor’s comment: if pressure is too low at only one machine, increasing the setpoint of all compressors should be the last response, not the first. First check whether the problem lies between the main line and the end use.
15. What should be included in the audit report?
The report should allow reconstructing the line of reasoning – from input data to conclusion. A mere list of recommendations without graphs and measurement bases is difficult to verify.
A well-prepared report should include:
- audit boundary and system configuration description;
- equipment inventory;
- list of meters used and measurement points;
- dates, recording period, and information on the representativeness of the period;
- relevant information on instrument accuracy, calibration, or verification;
- graphs of power, energy, flow, and pressure on a single timeline;
- compressor operating states;
- production data and description of plant operating mode changes;
- balance of compressor and auxiliary equipment operation;
- pressure drop analysis;
- assessment of required quality and dew point, if relevant;
- leak detection results, if performed;
- end-use analysis;
- an indication of whether the identified problem lies with generation, transmission, or demand;
- assumptions, limitations, and uncertainties;
- recommendations derived directly from measurements, without a preconceived solution.
For example, if a recommendation concerns changing the control of compressors, the report should show a profile that justifies this change. If the problem is the network, pressure drops at specific points and the flow conditions under which they occur should be visible.
16. Most common errors in compressed air audits
Basing conclusions solely on nameplates
The rated motor power and catalog efficiency do not indicate how the device performs in the actual plant profile.
Measuring pressure only in the compressor room
This does not allow separating the source problem from the distribution problem and local connections.
Lack of measurement synchronization
An energy chart from one day and a flow chart from another day may look similar, but they do not form a single balance.
Treating leak detection as the entire audit
Repairing leaks can reduce demand, but still leave improper control, unnecessarily high pressure, or large pressure drops in the network.
Rigid adherence to measurement duration
A “full week” is a good period only if the week truly represents the plant’s cycle. Otherwise, it may be too short or unnecessarily long.
Using universal reference values without conditions
Pressure drop, specific power, dew point, or idle run share must be evaluated within a specific system, at a defined pressure, flow, quality, and operating profile. A single number without reference conditions is rarely sufficient for an investment decision.
FAQ – Compressed Air Audit and Measurements
Is flow measurement required in every audit?
Direct measurement at every point is not always feasible, but flow is one of the most important parameters for evaluating system performance. If controller data, estimations, or other surrogate indicators are used, the report must clearly describe the method and its limitations.
How long should measurements last?
Long enough to cover a representative operating cycle. For a stable installation, this might be a relatively short period covering all states, while for a plant with variable production, longer recording will be needed. There is no single number of days suitable for all systems.
Is data from the compressor controller sufficient?
It can be very valuable, especially if it contains a history of power, pressure, efficiency, and operating states. However, it is necessary to check the definitions of parameters, how they are determined, and compare them with independent measurements where accuracy is critical for conclusions.
Is leak detection a compressed air audit?
It is one element of an audit. A full system assessment also covers generation, control, air treatment, the distribution network, pressure, flow and end uses.
When is dew point measurement necessary?
When the humidity of compressed air is critical for the process, product, equipment reliability, or specific quality requirements. In other installations, a full quality measurement may not be necessary to address the main energy problem.
Does lower compressor power mean higher efficiency?
No. Power must be related to the amount of air supplied, pressure, reference conditions, and operating state. A compressor consuming fewer kW may simultaneously deliver proportionally much less air.
Technical Basis and Current Standards
The following are particularly useful for evaluating compressed air systems:
- ISO 11011:2013 – Compressed air — Energy efficiency — Assessment – a published standard for assessing the entire system; as of August 21, 2026, it remains the current published edition;
- ISO/AWI 11011 – work on Edition 2 has begun; the project is currently at the preparatory stage and is not a published standard;
- ISO 8573-1:2010 – compressed air purity classes for particles, water, and oil;
- ISO 8573-3:1999 – methods for measuring compressed air humidity;
- ISO 1217:2009 with amendment from 2016 – acceptance test methods for flow and power demand of displacement compressors;
- U.S. DOE – Improving Compressed Air System Performance: A Sourcebook for Industry – a practical approach to building a baseline from power, flow, and pressure measurements and correlation with production;
- ORNL MEASUR – Compressed Air Assessments – tools for modeling the operation of compressors and compressed air systems.
Summary
A good compressed air audit is not a single measurement and does not begin by selecting equipment to modernize. First, build a reliable picture of how the system operates by aligning energy, flow, pressure, compressor operating states, air quality, end-use operation and production data on a common timeline.
Only this combined data set makes it possible to distinguish inefficient compressor operation from distribution-system restrictions, a local issue at an end use, or a genuine increase in production demand.
If the goal is to commission measurements and a full assessment of the system at the plant, the scope of work is described on our compressed air system audit page.