

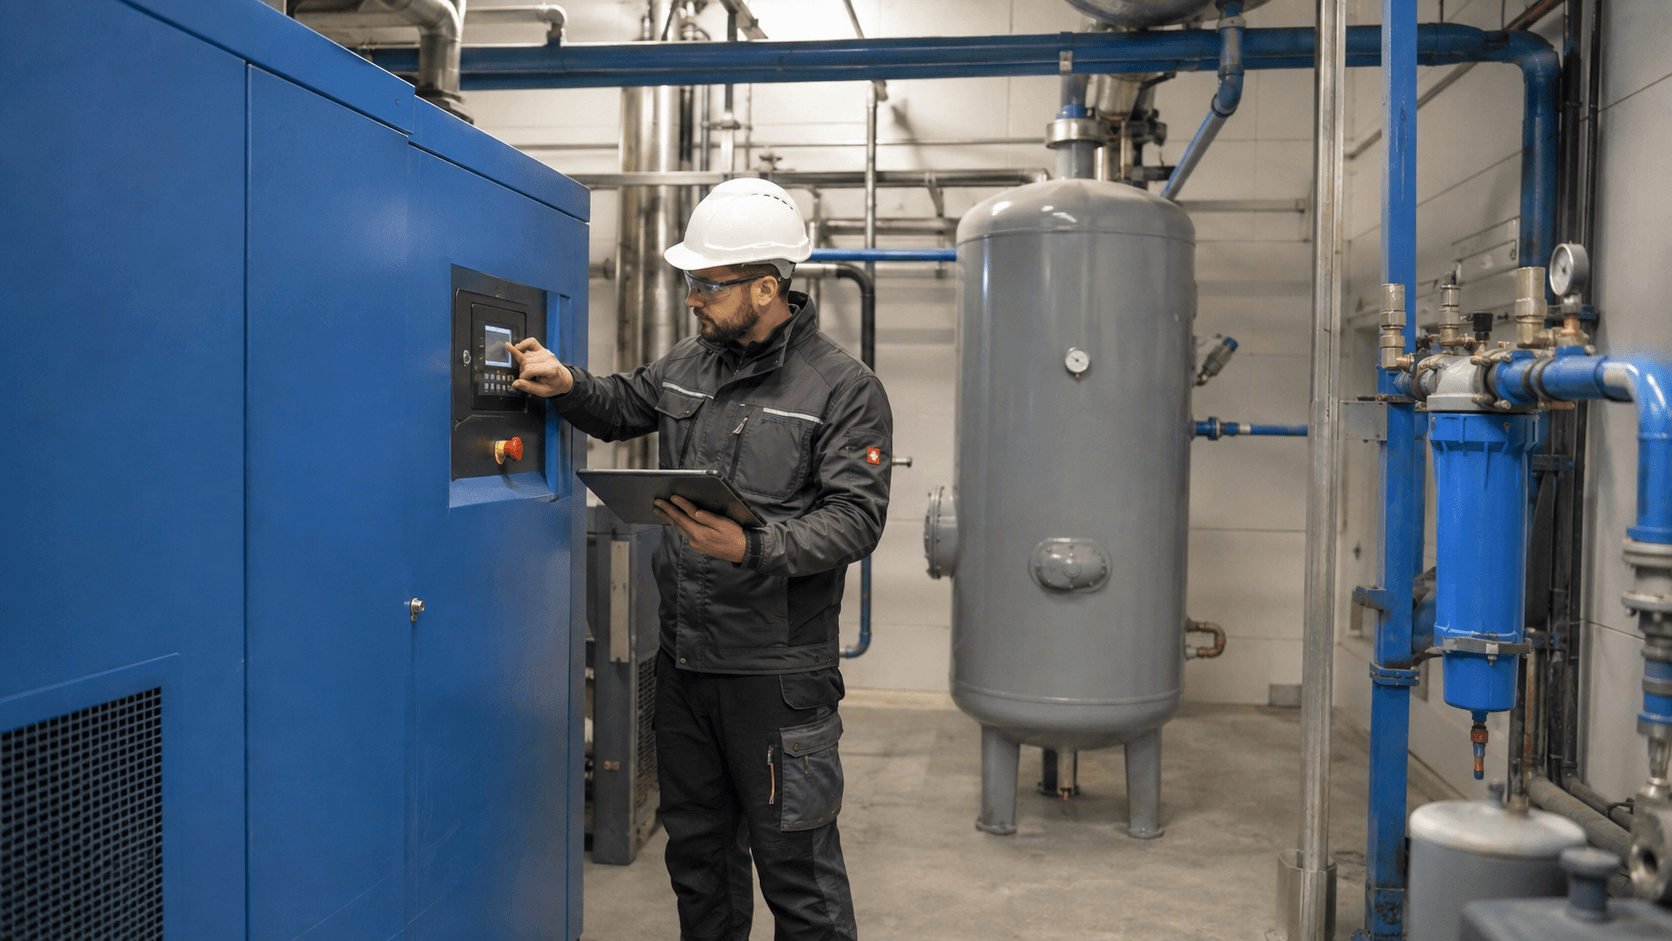
Compressed air is an energy system, not a single piece of equipment. A properly conducted audit therefore does not end with checking the compressors or finding leaks. It covers the entire chain: from electricity consumption and compressed-air generation, through treatment, drying, storage and distribution, to the parameters required by end-use equipment.
At Energy Trend, we tailor the audit scope to the installation, production profile and the problem that needs to be explained. We do not assume in advance that the answer will be a variable-speed drive, lower pressure, a larger air receiver or a compressor replacement. We first collect data and, where necessary, take measurements. Only then do we assess how the entire system works together and develop improvement options.
What does a compressed air system audit involve?
The purpose of the audit is to establish how the system actually operates: how much energy it uses, when and where demand for air arises, what pressure is available in different parts of the network, how the compressors and air-treatment equipment operate, and whether the delivered air parameters meet process requirements.
This approach follows the logic of ISO 11011, which treats a compressed air installation as a complete system – from energy input to the work performed by end uses – and divides the assessment into supply, transmission and demand.
In practice, an audit may include, among other things:
- analysis of compressor configuration and controls,
- electricity consumption profile and loaded/unloaded operating states,
- measurement or analysis of compressed air flow,
- pressure logging in the compressor room, distribution network and at selected points of use,
- assessment of dryers, filters, separators and pressure losses across air treatment,
- analysis of air receivers and their role in system stabilisation,
- assessment of the distribution network layout and local flow restrictions,
- pressure dew point measurement and – where required by the process – assessment of compressed air quality,
- leak detection as one module of the audit,
- analysis of the parameters and operating patterns of end-use equipment,
- development of improvement options with assumptions, priorities and – where the data allow – an assessment of the energy and economic impact.
The audit covers the entire system – from compressor to end use
1. Compressed air generation
The first area is the compressor room. Simply reading the compressors’ rated power does not show how much energy the system uses or whether the equipment operates efficiently. What matters is the actual load profile, the control method, load/unload pressure setpoints, the operating sequence of multiple compressors and how the system responds to changing plant demand.
As part of the audit, we check, among other things:
- the number, type, power and capacity of the compressors,
- the control method: load/unload, capacity control, variable-speed drive or master control,
- total running hours, loaded hours and unloaded hours, where the controller provides such data,
- power or energy profile over time,
- discharge pressure and control range,
- how the compressors interact at different demand levels,
- cooling and air-intake conditions,
- the potential to use waste heat where technically and economically justified.
It is essential to distinguish equipment capacity from the efficiency of the overall system. A compressor may be technically sound while the system still consumes too much energy because of poor control, long periods of unloaded operation, high pressure losses or demand originating at the end-use side.
2. Air treatment and drying
Compressed air usually passes through separators, filters and dryers. Each component has a specific air-quality function, but it also affects flow resistance and the operating conditions of the entire system.
We verify whether the treatment method matches the actual process requirements, whether filters and dryers create excessive pressure drops, and whether their operating parameters meet end-use needs. Depending on the drying technology, the assessment may also cover regeneration method, compressed air used for the dryer’s own operation or auxiliary energy consumption.
We do not assume that “better” air quality always means a better system. The required purity level should follow from the process, product and equipment requirements, and the treatment system should deliver those parameters without unnecessary losses.
3. Compressed air receivers
An air receiver is not merely an air storage vessel. Its volume and location can affect pressure stability, the frequency of compressor state changes and the system’s ability to cover short-term peaks in demand.
During the audit, we analyse the role of air receivers in the specific system: their location relative to sources and end uses, how they are connected to the network, system behaviour during sudden demand peaks, and whether the issue is genuinely insufficient storage or, for example, restricted capacity in piping or fittings.
4. Distribution network and pressure drops
Pressure at the compressor is not the same as pressure available at the machine. Losses can occur across filters, dryers, pipes, valves, quick couplings, pressure regulators and local branches.
For this reason, the network assessment is not limited to the diameters of the main pipework. We check, among other things:
- the arrangement of headers, ring mains and branches,
- diameters and lengths of critical sections,
- locations with high or variable flow,
- valves, fittings and connections that restrict capacity,
- pressure differences between the compressor room and the ends of the distribution network,
- pressure behaviour during peak demand,
- inactive or unnecessary sections of the installation,
- the potential for local storage or separation of end uses with different requirements.
Where pressure problems occur, it is important to measure several points at the same time. A single pressure gauge may show a correct value in the compressor room while short-term pressure drops at an end use remain invisible.
5. End uses
The final stage of the audit is where compressed air actually performs useful work. For selected end uses, we determine the required pressure, flow demand, operating time and operating pattern, as well as air-quality requirements.
The assessment may cover cylinders, pneumatic tools, nozzles, blow-off applications, conveying systems, valves, vacuum systems generated using compressed air and other process applications.
The demand side often explains why the entire plant maintains a certain pressure or why demand rises sharply for short periods. Without understanding end-use requirements, it is not possible to decide reliably whether source parameters should be changed, the network rebuilt, local regulation introduced or the current settings retained.
What data and measurements may be needed?
There is no single measurement package that is identical for every installation. The scope should follow from the audit question, the available data and the plant’s operating characteristics. Measurements should reconstruct a representative system profile, not simply collect as much data as possible.
| Data or measurement | What it helps assess |
|---|---|
| Compressor electricity and power | Actual energy consumption, load variability and compressor operation over time |
| Compressor operating states | Share of loaded operation, unloaded operation and downtime, and how the system responds to demand |
| Compressed air flow | Demand profile, peak consumption, differences between production shifts and the relationship between air production and energy use |
| Pressure | Pressure level at the source and in the network, stability, dynamic pressure drops and conditions available at points of use |
| Pressure dew point | Drying performance and the ability to meet process moisture requirements |
| Oil and particle content | Compressed air quality where process requirements justify such testing |
| Leak detection | Location of loss points and a list of locations for repair; quantitative assessment of the impact requires an appropriate method and operating data |
| End-use parameters | Minimum required pressure, flow, duty cycle and air quality for the process |
| Production data and operating schedule | Distinguishing changes caused by production from changes caused by the way the installation is operated |
Where flow is logged, the documentation should clearly state the unit and reference conditions. m³ and Nm³ should not be compared directly without information about the conditions to which the measurement refers. Similarly, gauge pressure and absolute pressure must be distinguished.
How long should measurements run and how frequently should data be logged?
We do not automatically assume that every audit requires exactly one week of measurements. The logging period should cover representative operating states of the installation.
A plant operating in a stable, repeatable mode may require a different measurement period from a business with several shifts, weekend production, frequent changeovers or large differences between production batches. If shutdown periods or off-production demand are relevant, the measurements should cover those periods as well.
Before logging starts, we therefore identify which operating modes need to be visible in the data. Only then do we select the measurement duration, logging interval and sensor locations.
Electricity and compressor operating profile
Energy measurements should be analysed together with what is happening on the compressed air side at the same time. A kWh figure alone does not explain whether the issue is excessive demand, control strategy, unloaded operation, pressure drops or poor interaction between multiple compressors.
In practice, it is particularly valuable to place the following on a common time axis:
- electrical power or energy,
- flow,
- pressure at selected points,
- operating states of individual compressors,
- information about the production shift or process state.
Only such a combined view reveals the relationships. For example, if one compressor runs unloaded for long periods, this does not automatically mean it should be replaced with a variable-speed machine. First, the demand profile, settings of the other compressors, available storage volume and pressure behaviour need to be checked.
Pressure measurement – why is the compressor setpoint alone not enough?
A high pressure setpoint at the compressor may be the result of a problem elsewhere in the installation. Possible causes include local restrictions, contaminated air-treatment components, an unsuitable network configuration, a short-term high-demand end use or leaks that increase total flow.
A recommendation to reduce pressure should therefore only be made after confirming:
- the minimum pressure actually required by the end uses,
- the pressure drops between the source and points of use,
- how the installation behaves at peak demand,
- whether changing the setpoint would compromise process stability,
- how the change would affect compressor operation and controls.
In an audit, we do not apply a fixed rule such as “reducing pressure by a given amount always delivers a given percentage saving”. The effect depends on the specific characteristics of the system and must be assessed from data.
Compressed air flow
Flow measurement shows how much air the system supplies in different periods and how demand changes. It is particularly useful when analysing multiple compressors, comparing production shifts, assessing off-production consumption and verifying selected end uses.
The measurement point must be selected for the purpose. A measurement on the common compressor-room header provides different information from a measurement on a department branch or directly upstream of an end use. In extensive systems, parallel monitoring of several zones may be appropriate.
Flow results are always interpreted together with pressure, process status and the measurement device’s reference conditions. A flow reading without production context can lead to incorrect conclusions.
Dew point and compressed air quality
A system-efficiency audit and compressed air quality testing are related but separate subjects. Not every installation requires a full set of air-purity measurements as part of every audit.
Where air quality matters to the product or process, the scope may include pressure dew point and testing for particles and oil. ISO 8573-1 classifies compressed air purity with respect to, among other things, particles, water and oil, while the relevant parts of the ISO 8573 series describe measurement methods for individual contaminants.
From an audit perspective, two questions need to be considered together: what air quality the end use actually requires and what energy and operating cost the installation incurs to deliver that quality. Dew-point or air-quality measurements should therefore follow from process needs and the purpose of the audit, rather than being performed mechanically at every site.
Leak detection versus a full compressed air system audit
Leak detection is an important part of improving efficiency, but it does not answer every question about how the installation operates.
| Leak detection | Full system audit |
|---|---|
| Focuses on locating leaks | Analyses the source, air treatment, storage, distribution network and end uses |
| Produces a list of points to repair | Explains how the whole system interacts and what causes the losses |
| Can be performed as a standalone service | Can include leak detection as one of its modules |
| Does not require a full analysis of compressor controls | Assesses compressor controls, loading and interaction |
| Does not replace energy, pressure and flow profiling | Combines measurements and operating data into a single diagnostic balance |
| A good choice when the objective is a list of leaks to eliminate | Appropriate when the aim is to determine why the system uses too much energy or fails to deliver the required parameters |
If the sole objective is to find and document leaks, the appropriate service is compressed air leak detection. If the problem concerns energy use, controls, pressure stability, network capacity, air quality or end-use operation, leak detection alone does not replace a full audit.
Are a variable-speed drive, lower pressure or compressor replacement the solution?
They may be – but only if the data support them.
A variable-speed compressor can respond well to changing demand in a specific role within the system, but it is not automatically the best solution for every compressor room. Similarly, master control can improve the coordination of several compressors when sequencing is the issue, but it will not remove a flow restriction at the far end of the production hall.
Reducing pressure can lower energy demand, but only within limits that allow end uses to operate correctly. If high pressure in the compressor room is compensating for a large drop across a filter, a restriction or an undersized connection, the first step may be to remove that restriction rather than change the setpoint.
Replacing a compressor makes sense when the analysis shows that the existing unit is mismatched, worn or unable to serve the actual operating profile efficiently. In other cases, greater benefits may come from correcting the controls, repairing leaks, rebuilding part of the network, changing how compressed air is used or improving storage.
A recommendation is the outcome of the audit, not its starting assumption.
How are recommendations developed after the audit?
Every action should be linked to an identified problem and to the data that confirm it. This is why the report separates observations from recommendations.
Example: if short-term pressure drops occur in one department, we do not immediately assume that pressure should be increased across the entire plant. We check the pressure profile in the compressor room and at the end use, the flow profile, the condition of valves and fittings, the connection diameter and when the peak occurs. Only then can we assess whether the right solution is a network modification, a local air receiver, a change in demand sequence, local regulation or intervention at the source.
Typical groups of measures that may be analysed include:
- adjusting compressor sequencing and control setpoints,
- reducing unloaded operation,
- matching the source configuration to the actual demand profile,
- repairing leaks,
- reducing unnecessary or inefficient uses of compressed air,
- reducing pressure losses in air treatment, piping and valves,
- separating end uses with different pressure requirements,
- local regulation or storage for peak-demand end uses,
- changing the drying or filtration method where the current system is mismatched to requirements,
- upgrading or replacing a compressor where justified by the operating profile and system condition,
- using master control or variable-speed control where this matches the demand characteristics,
- heat recovery from compressors where there is a useful heat sink and suitable operating conditions,
- continuous energy monitoring and management in installations where continuous tracking of parameters is justified.
Not every installation needs every one of these measures. Part of the audit is to establish the sequence and justification for intervention.
What does the audit report contain?
The report scope depends on the agreed measurement scope, but it should enable a clear path from data to a technical decision. The report may include:
- a description of the installation configuration and audit boundaries,
- a summary of compressors, dryers, filters, air receivers and significant network components,
- a description of the plant operating profile and measurement conditions,
- charts of energy, power, flow and pressure where these parameters were logged,
- analysis of compressor operating states and interaction,
- identification of significant pressure drops and capacity restrictions,
- dew-point or air-quality measurement results where included in the scope,
- leak-detection results where leak detection formed part of the audit,
- assessment of selected end uses,
- a list of identified problems supported by measurement evidence,
- options for corrective and modernisation measures,
- implementation priorities and dependencies between measures,
- estimates of energy and economic impact where data quality, baseline conditions and the adopted methodology allow,
- assumptions, limitations and an indication of the data worth monitoring after changes are implemented.
The report should not be limited to a shopping list of equipment. Its value lies in showing why a particular change is recommended and what conditions must be met for the expected result to be achievable.
When is a full audit worthwhile?
A full audit is particularly useful when:
- energy consumption in the compressor room is high or increasing, but the cause is unknown,
- several compressors operate in the installation and it is unclear whether their controls are properly coordinated,
- pressure drops or fluctuations occur at end uses,
- the plant is planning to expand production and system reserve capacity needs to be verified,
- there is a question about replacing a compressor, buying a variable-speed unit or changing the control system,
- it is unclear whether drying and filtration meet process requirements,
- the installation has been expanded repeatedly and there is no current picture of flows and restrictions,
- leaks have already been repaired but energy consumption remains too high,
- baseline parameters need to be established before a modernisation and a method is needed to verify the effect afterwards.
If the problem is known and limited to locating leaks, a full audit may be unnecessary. In that case, a standalone leak-detection service is the better option.
Standards and assessment methodology
For a compressed air system assessment, ISO 11011 can be used as a reference. It sets out requirements for assessing the energy performance of the entire system, analysing data and reporting the results.
Where the subject of testing is compressed air purity, ISO 8573-1 defines purity classes for particles, water and oil, while other parts of the series describe the relevant measurement methods. The scope of such testing should follow from process requirements.
ISO 50001, by contrast, is an energy management system standard and is technology-neutral. It does not prescribe a specific solution for the compressor room and does not provide a basis for automatically selecting a variable-speed drive, pressure level or compressor type.
How should you prepare for the audit?
At the outset, basic information about the installation and the problem to be analysed is sufficient. Where available, the following are useful:
- a list of compressors with their basic parameters and controls,
- information on dryers, filters and air receivers,
- an installation diagram or current plant layout,
- production and shift schedule,
- data from energy meters or compressor controllers,
- information on typical and maximum pressure values,
- a list of end uses with particularly high or critical demand,
- dew-point and compressed air quality requirements,
- history of problems, failures and previous modernisations.
Incomplete documentation does not prevent an audit. Some data can be collected during the site visit and measurements. What matters is to define the system boundaries, a representative operating period and the questions the audit is intended to answer before logging begins.
Define the scope of your compressed air system audit with us
We tailor the scope to the size of the installation, number of compressors, plant operating pattern, available data and the objective of the analysis. It may be a diagnosis of a specific problem or a comprehensive assessment of compressed air generation, treatment, distribution and use.
Contact Energy Trend to describe your installation and determine what data and measurements will be needed to prepare the audit.