

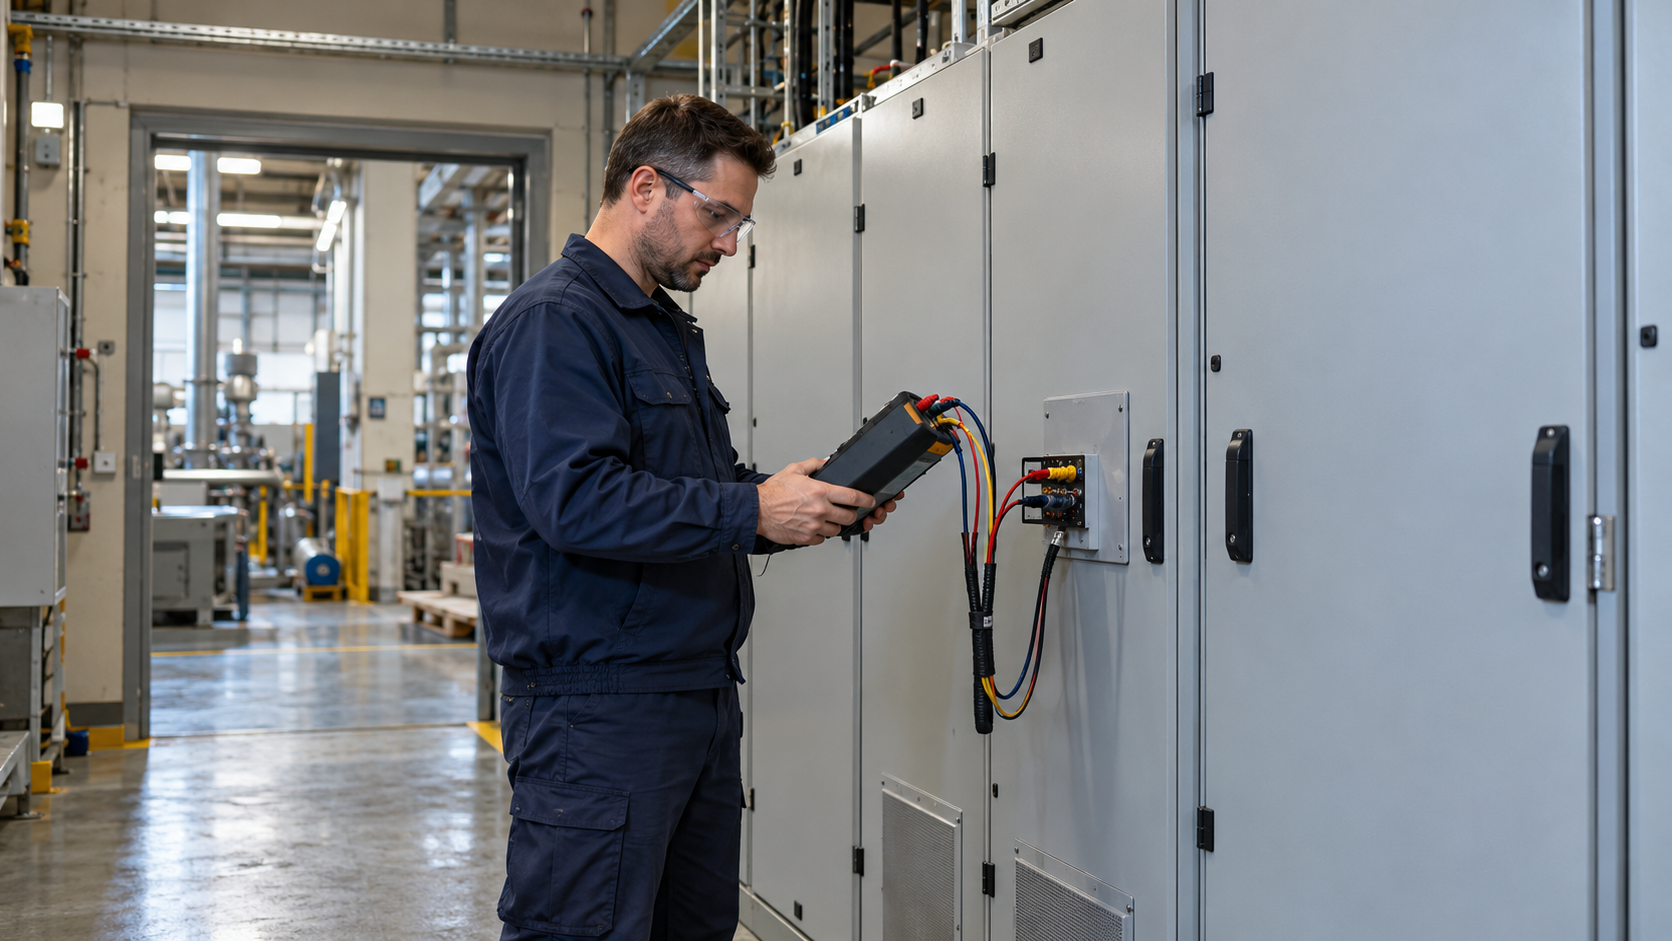
Power quality directly affects production reliability. A brief controller shutdown, flickering lights or overheating components may be related to the power supply, but the symptom alone does not establish the cause. To distinguish a grid disturbance from a problem within the facility, examine the event timing, operating equipment and relevant recordings together.
What does power quality mean?
Power quality concerns the characteristics of the supply voltage and phenomena that can disrupt equipment: voltage dips, interruptions, fluctuations, unbalance, waveform distortion and transient overvoltages. Diagnostics also examine the currents drawn by equipment, which can help identify disturbance sources. An overview of the main phenomena is provided in the technical guide published by Poland’s Office of Technical Inspection (UDT).
For an industrial facility, it helps to separate three questions:
- Is electricity supplied with the required characteristics? This concerns voltage quality and supply continuity at a specified point in the network.
- How much energy does the process use? The answer comes from kWh, load profiles and production data; these do not, on their own, assess voltage waveform quality.
- What is the company paying for? The bill shows electricity purchase and distribution costs and any reactive energy charges, but it does not record brief disturbances.
High energy consumption in kWh does not automatically imply poor power quality. Conversely, a low-consumption facility can experience brief dips that stop sensitive automation. If the question concerns the bill, a starting point is an analysis of the electricity distribution bill. If equipment resets or lights flicker, a different set of data is needed.
Which power quality parameters matter in industry?
No single indicator answers every question. The importance of each parameter depends on the type of equipment, the measurement location and the event duration.
| Parameter or phenomenon | What it describes | Why it may matter |
|---|---|---|
| Voltage magnitude and variations | Voltage level, deviations and rapid changes | May affect power supplies, automation and visible fluctuations in lighting brightness. |
| Voltage dip, swell and interruption | The event, its depth or residual voltage, and its duration | A short event may stop a process while average energy consumption remains virtually unchanged. |
| Voltage and current harmonics | Waveform distortion relative to the fundamental component, including the spectrum and THD indices | May be associated with additional currents, heating and interactions with power-electronic equipment. |
| Voltage unbalance | Unequal voltages and phase relationships in a three-phase system | Can impair the operating conditions of some three-phase equipment. |
| Light flicker and rapid voltage changes | Repetitive or step changes in voltage, described in part by Pst and Plt | Help correlate observed flicker with the operation of variable loads. |
| Frequency and transient overvoltages | Deviations in grid frequency and very short voltage events | Require separate recording methods; not all will appear on an RMS voltage chart. |
An important distinction between standards: EN 50160:2022 with Amendment A1:2025 covers the main voltage characteristics at the point of supply from public electricity networks under normal operating conditions. In Poland, the corresponding standard is PN-EN 50160:2023-10, with Amendment A1:2025-04 published subsequently. Industrial networks are outside the standard’s scope. Consequently, measurements at the terminals of an arbitrary machine cannot automatically be assessed in the same way as measurements at the point of supply.
A separate electromagnetic compatibility framework applies to internal distribution systems in industrial facilities, including IEC 61000-2-4:2024. This standard specifies compatibility levels at in-plant points of coupling. Technical standards do not replace connection conditions, the agreement with the network operator, the requirements of specific equipment or an assessment of installation safety.
How should symptoms be interpreted before commissioning measurements?
A symptom is a clue, not a diagnosis. The same failure may be caused by voltage disturbances, a poor contact, an unsuitable control power supply, an equipment fault or incorrect protection settings.
| Observation | Possible areas to investigate | What to collect first |
|---|---|---|
| Controller reset or contactor dropout when a large load starts | Brief voltage dip, voltage drop in the local control circuit, power supply problem | Event time, PLC/UPS alarms, start-up time, supply circuit |
| Lighting flicker during cyclic machine operation | Rapid voltage changes, large current variations, shared supply path | Cycle schedule, extent of flicker, voltage change recordings |
| Overheating transformer, cables or capacitor bank | Load, current harmonics, unbalance, poor connections or a fault | Phase currents, load, thermogram/inspection by qualified personnel, protection data |
| Inverter, UPS or power supply alarms | Dips, swells, transients, faults in the equipment itself or incorrect settings | Alarm code, equipment documentation, simultaneous events |
| Only one machine is affected | Local circuit, switching equipment, power supply or the load itself | Single-line diagram of the branch, service history, measurements at its supply point |
If there are signs of overheating, the smell of damaged insulation, arcing or repeated protection trips, safety takes priority. Assessment and work inside switchgear should be carried out by appropriately qualified personnel. Power quality diagnostics are no substitute for inspection of the installation’s technical condition or protection against electric shock.
Does the problem originate in the operator’s network or within the facility?
Neither a single chart nor the statement that “voltage is within limits” can settle this. You need to know where the measurement was taken and what was happening in the installation when the disturbance occurred.
The point of supply, switchboard and load are different locations
The point of supply is used to assess conditions at the interface with the external network against the applicable requirements. The main switchboard shows conditions on the facility side, while recording closer to a particular load helps identify voltage drops and disturbances arising in that branch.
When measurements from several points share a common time base, it is possible to check whether a phenomenon is already present upstream or only appears farther into the installation. Without synchronization, distinguishing a cause from a coincident event is harder. The comparison must also account for the installation topology, switching states and loads being started.
Voltage and current answer different questions
Voltage at the measurement point describes the supply conditions experienced by loads. Current helps identify loading, starts, load unbalance and disturbances emitted by equipment. High current distortion from one inverter is not, by itself, evidence that voltage quality limits have been exceeded at the point of supply. Similarly, a normal voltage record at the connection point does not rule out a problem in a remote circuit.
Where converters are suspected, the analysis should extend beyond aggregate THD to include the harmonic spectrum, measurement location and operating conditions as relevant. Installing a filter or adjusting compensation is a separate decision. Reactive power charges alone are not evidence of poor voltage quality; our guide to reactive power compensation discusses billing and possible measures in more detail.
What can a bill, a 15-minute profile and a fault log reveal?
Each data source answers a different question. What connects them is the timing and location of measurement, not simply the presence of electrical values.
| Data | What it tells us | What it usually cannot show |
|---|---|---|
| Invoice and billing data | Consumption in kWh, certain cost components, reactive energy and billing periods | Momentary voltage dips, overvoltages and voltage waveforms |
| Power or energy profile at 15-minute intervals | Load patterns, aggregated peaks and relationships with shifts and work schedules | A brief event lasting a fraction of a second |
| PLC, UPS, inverter and protection logs | Alarm time, code, machine state and sequence of events | Voltage parameters outside the recording capabilities of the device |
| Power quality recorder selected for the task | Voltage events, waveform parameters and, depending on the instrument, time-domain waveforms | Automatic identification of who is responsible without installation and process context |
A power chart with 15-minute intervals may show that an energy-intensive process started before a failure. It cannot establish whether voltage fell below the controller’s immunity threshold for 0.2 seconds. That requires data with sufficient time resolution.
IEC 61000-4-30:2025 provides the basis for comparable measurement methods. It defines, among other things, Class A and Class S methods and how different power quality parameters are observed. The choice of class, locations and recording duration depends on whether the aim is to assess conditions at the point of supply or find the cause of an in-plant stoppage. An instrument labelled “power quality analyzer” does not necessarily capture the particular event you need.
Example: a momentary voltage dip during machine start-up
Suppose a controller stops an industrial process when a large load starts. A recorder at a local switchboard captures a drop in line-to-line voltage from an assumed reference of 400 V to 320 V lasting 0.2 s. In this illustrative event:
Relative voltage drop = (400 V – 320 V) / 400 V × 100% = 20%. The residual voltage is 80% of the assumed reference level.
This calculation describes the event but does not prove that it caused the reset. First check the actual controller power supply’s immunity, its logs and the conditions in the control circuit. Then compare recordings at the main switchboard and at the load, together with the starting current.
If the dip is visible in only one branch, investigate that branch’s impedance, connections and loading. If a similar event appears at several points, examine the shared supply path and conditions at the point of supply. Neither scenario, without further data, is enough to assign responsibility to the network operator or justify purchasing a particular device.
How can further diagnostics be matched to the problem?
From an auditor’s perspective, the sequence of work should follow the observed symptoms and the risk of downtime.
- Define the event. What stopped working, how long did the problem last and when did it occur? Was it a one-off or does it recur at the same point in a cycle?
- Determine the extent. One machine, one switchboard or several production halls? Mark the affected circuits on a single-line diagram.
- Synchronize the available records. Compare alarms from PLCs, UPS units, drives and protective devices, and the maintenance log, with the production schedule. For inverter-related problems, information on electric motors and drives can also help.
- Match the measurements to the question. Confirming voltage conditions at the point of supply requires a different scope from investigating a local shutdown. Decide which operating states and installation points need to be recorded. If the event is rare, a short measurement at an arbitrary time may miss it.
- Only then assess solutions. Repairing a local fault or correcting a control circuit may be sufficient. Sometimes the installation needs modification, coordination with the distribution system operator in Poland (OSD), or a measure that addresses a specific disturbance. Technology should be selected based on the cause, not on the general label “poor power quality”.
Where the issue concerns the quality of supply from the public network in Poland, document the events and follow the relevant network operator’s procedure. The Polish Energy Regulatory Office (URE) explains that power quality checks are handled separately from ordinary billing complaints. Observations at a load cannot replace an assessment at the required point.
What information should you prepare for a power quality discussion?
You do not need a complete set of measurements to get started. The most useful information includes:
- a brief description of the symptom and its effect on production, with dates and event times as accurately as possible;
- a list of the affected equipment and circuits, including alarm codes;
- an available single-line diagram or a description of the supply path, transformers and switchboards;
- whether events coincide with start-up, shutdown or changes in the load of particular machines;
- existing logs, voltage/current recordings, load profiles and maintenance system data;
- a list of recent changes to the installation, loads, compensation equipment and on-site sources.
An initial assessment should answer three questions: what do we actually know, what remains unknown, and which measurement or check will most quickly distinguish between possible causes? This reduces the risk of investing in equipment that will not solve the problem.
If your facility experiences recurring shutdowns, flicker or unexplained alarms, send Energy Trend a description of the situation and the available data using our contact form. This will help establish what information is needed to determine the next diagnostic steps.
Technical and official sources
- Austrian Standards – EN 50160:2022+A1:2025 (public networks; adopted in Poland as PN-EN 50160:2023-10 with Amendment A1:2025-04).
- IEC 61000-2-4:2024 – compatibility levels in internal distribution systems at industrial sites.
- IEC 61000-4-30:2025 – power quality measurement methods (fourth edition, corrected version of July 2026).
- Poland’s Office of Technical Inspection (UDT) – technical guide, section 7.2.2 on phenomena affecting power quality.
- Polish Energy Regulatory Office (URE) – complaints and power quality checks.