

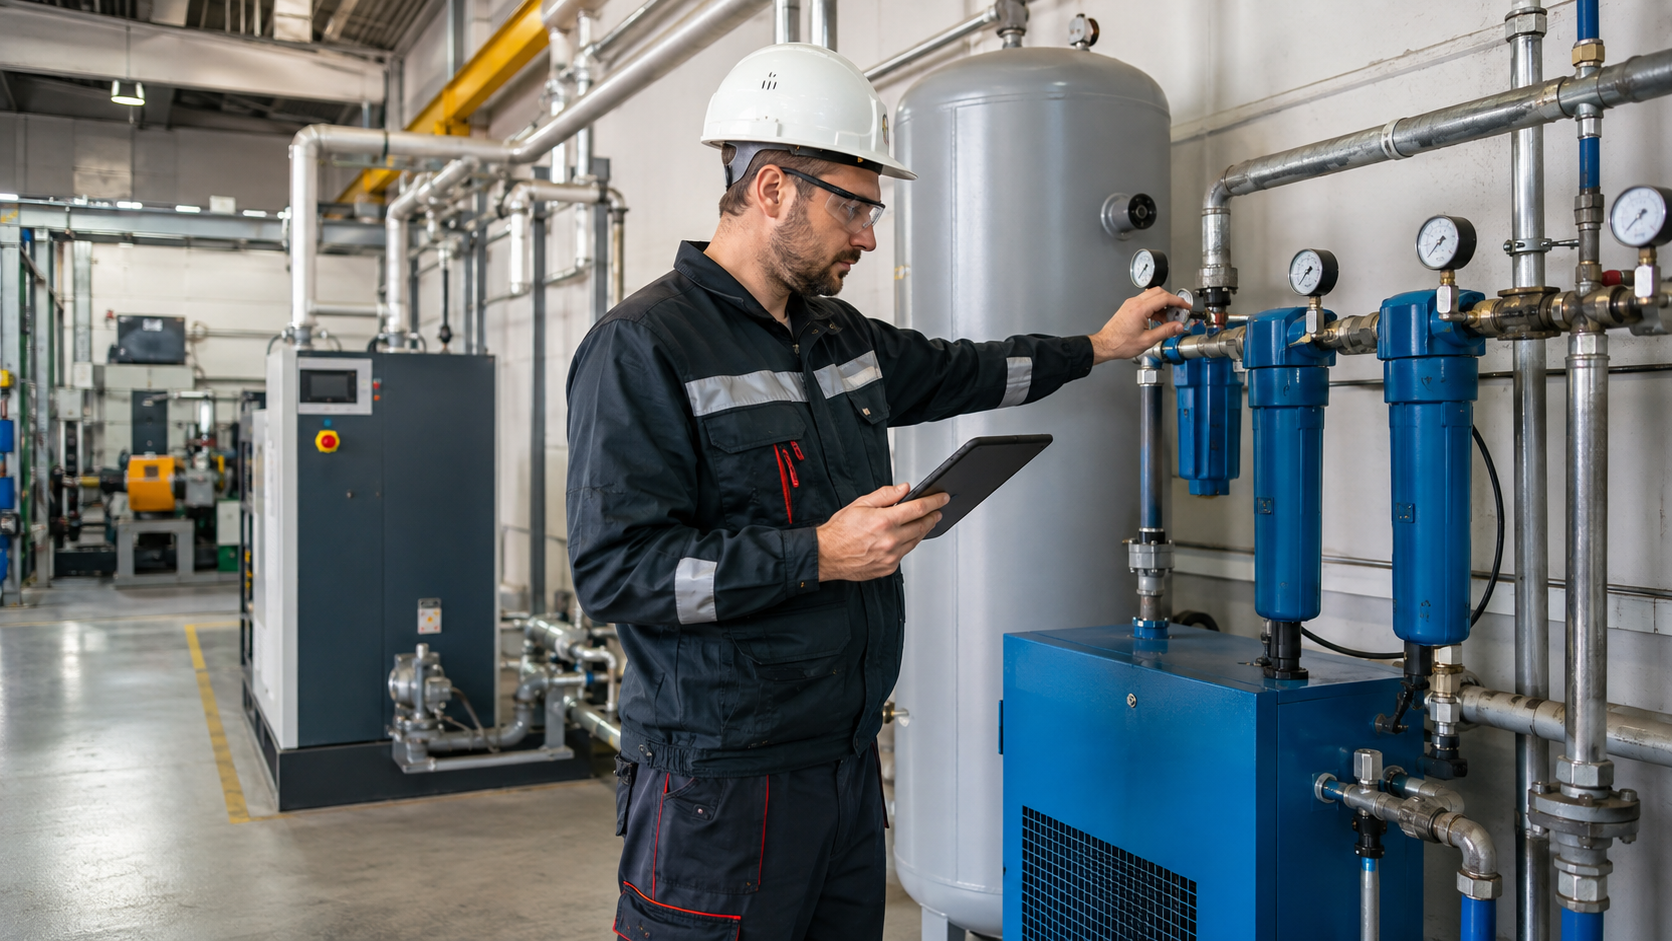
Compressed air system optimization should not start by asking which compressor to buy or by automatically reducing pressure. First, determine how much air the plant actually needs, when demand occurs, and what pressure and air quality are required at the points of use. Only then can the entire system be traced – from generation, through treatment and distribution, to the way compressed air is used – and the actions put in the right order.
A common mistake is to treat the symptom rather than the cause. A pressure drop at a machine does not necessarily mean the compressor is undersized, high energy consumption does not necessarily mean the compressor is worn out, and a large number of leaks does not automatically explain all losses. In a compressed air system, the source, controls, receivers, treatment equipment, piping and end uses all interact.
In brief: where should compressed air optimization begin?
A practical analysis sequence is as follows:
- determine actual demand and the flow profile;
- check the operation of each compressor and how it is controlled;
- separate loaded operation, unloaded operation and part-load operation;
- determine the required and actual pressure;
- measure pressure drops in the distribution network and across treatment equipment;
- assess air receivers and the ability to buffer short demand peaks;
- check drying, filtration and the air quality actually required;
- determine the scale of leakage;
- analyse end uses and so-called artificial demand;
- only then compare control strategies, compressor configurations and infrastructure changes;
- assess heat recovery separately.
This is the diagnostic sequence. It does not mean an obvious leak should be left unrepaired until stage eight. The point is that investment decisions should be based on a picture of the entire system rather than on a single observation.
Why should the whole system be analysed rather than the compressor alone?
ISO 11011 takes a system approach to assessing the energy performance of compressed air: from energy input through to the work performed by end uses. The standard divides the system into three functional subsystems – supply, transmission and demand. This is an important practical principle: even a highly efficient compressor can operate within an inefficient system if pressure is set too high, the controls of several units conflict, the distribution network has excessive resistance, or end uses consume more air than the process requires.
As of 21 August 2026, ISO 11011:2013 remains the current published edition. In August 2026, ISO began work on the next edition, but it is not yet a published standard. Likewise, ISO 8573-1:2010 remains the published reference for compressed-air purity classes while work on a new edition is under way.
From an auditor’s perspective, it is useful to separate two questions. The first is: is the compressor in good working order and correctly sized? The second – much more important for the cost of the entire system – is: does the plant produce exactly as much compressed air as it needs, at the required parameters and at the lowest reasonably achievable energy cost?
Analysis sequence – 11 stages from demand to heat recovery
| Stage | What needs to be determined | Key data and measurements | Typical decision after analysis |
|---|---|---|---|
| 1. Demand | How much air the plant actually needs and when | flow, production schedule, machine states, production data | baseline for subsequent decisions |
| 2. Compressors | Which units operate and how they are controlled | power, energy, pressure, controller logs, capacity | assessment of the source configuration |
| 3. Loading | How long compressors produce air and how long they consume energy without useful flow | load/unload, VSD, instantaneous power, hours in each operating state | adjustment of sequencing and operating ranges |
| 4. Pressure | What pressure the process requires and what pressure the system actually maintains | pressure at the source and at points of use | reduce setpoints or remove the cause of the high setpoint |
| 5. Pressure drops | Where pressure is lost | simultaneous pressure logging at several points | maintenance, modification of the distribution network or valves and fittings |
| 6. Buffering | Whether short peaks require an additional compressor | flow, pressure, peak duration, receiver capacity | change storage capacity or its location |
| 7. Air quality | What level of dryness and purity the process requires | dew point, pressure drops, dryer and filter data, quality testing where required | match treatment to requirements |
| 8. Leaks | What flow does not perform useful work | leak detection, non-production flow, operating time | repair plan and verification of results |
| 9. End uses | Where air is used unnecessarily or at excessive pressure | local flow, pressure, duty cycle, regulator settings | reduce artificial demand |
| 10. Configuration | How to combine actions into one system-level option | all synchronized data | controls, network, receivers, VSD, compressor replacement – if justified |
| 11. Heat | Whether compressor heat has a useful heat sink | loaded power, operating hours, temperatures, heat-demand profile | heat recovery as an additional benefit |
1. Start with actual demand and the flow profile
The first question should not concern the installed compressor capacity. The task is to determine how much compressed air the plant actually consumes over time. A daily average is not sufficient if the system experiences short, high peaks or large differences between production shifts.
The most useful approach is to log flow and correlate it with the operating schedule. At a minimum, the data should show the base level, typical load, short-duration maxima, start-up and changeover periods, shutdowns and – where possible – non-production consumption. In a large system, it can be useful to split the main flow by department or group of end uses if the investment decision depends on it.
Production data are just as important as flow itself. If the plant produces twice as much output on one day, higher air consumption may be entirely justified. It is therefore useful to compare, for example, m³ of compressed air per tonne, item, batch or hour of actual process operation, depending on the nature of production.
Example: a plant has a short pulse demand that raises flow far above the baseline for several seconds. Selecting an additional compressor solely for this maximum may be premature. First check the peak duration, the permissible pressure drop and whether the pulse can be supplied from a correctly located air receiver.
2. Then assess each compressor and its controls
Only once demand is known can the sources be assessed meaningfully. For each compressor, collect the machine type, capacity at a specified pressure, total package input power, control method, pressure range and the logic governing its interaction with the other units.
Motor nameplate power alone is not enough. Two compressors with similar power ratings may deliver different flows at the same pressure and have completely different part-load characteristics. Standardized performance data, such as CAGI data sheets based on testing in accordance with ISO 1217, are useful when comparing equipment. However, parameters must be compared at the same pressure and flow conditions or correctly adjusted to equivalent conditions.
Controller logs are particularly important in an existing compressor room: pressure setpoint, load and unload pressures, total operating hours, loaded hours, share of variable-speed operation, number of starts and any fault states. If the controller does not provide reliable data, independent power and pressure logging is required.
3. Loaded, unloaded and part-load operation
A compressor does not consume energy only when it is effectively producing air. Depending on its design and control method, it may also draw significant power while unloaded or operate inefficiently at part load. A single universal percentage should not be applied to all types of equipment – actual power draw should be measured or obtained from reliable manufacturer data.
In a system with several compressors, check whether the units operate with overlapping pressure bands. A common situation is two machines running simultaneously in an unfavourable range even though one could cover the base load and the other could serve as the trim compressor. Another problem may be frequent unloading caused by insufficient storage volume or poorly set control thresholds.
A variable-speed compressor is not automatically the best answer either. Its role must be matched to the demand profile and its interaction with fixed-speed units. First determine what portion of demand is base load, what portion is variable, and over what range modulation is genuinely required.
4. Required and actual pressure
What matters in the system is the pressure available at the point of use, not only the setpoint in the compressor room. The analysis therefore begins by determining the process’s minimum requirements: what pressure must be available to a cylinder, tool, valve, nozzle or other critical end use during the actual operating cycle.
Only then should this be compared with pressure in the compressor room and distribution network. If the compressors maintain a high setpoint only because there is a large pressure drop at the far end of the plant, lowering pressure without removing the restriction may worsen the process. Conversely, increasing system-wide pressure because of one end use can increase demand elsewhere, especially where flow is not well regulated.
Do not use the rule “1 bar less = always X% savings”. The effect depends on compressor type, controls, actual flow, the characteristics of end uses, the level of leakage and whether power consumption actually decreases after the pressure reduction. The conclusion should follow from measurements and equipment performance characteristics.
5. Pressure drops in the distribution network and treatment equipment
If pressure at the compressor is correct but an end use has a problem, the point at which the pressure drop occurs must be found. Simultaneous pressure logging helps distinguish permanent losses from dynamic losses that appear only at high flow.
Measurement points should be selected for the actual system, but typically it is useful to compare pressure at the compressor outlet, before and after treatment equipment, on the main header, in a remote part of the network and immediately upstream of a critical end use. Where a filter, dryer or separator is suspected, measuring differential pressure directly across the component is also useful.
The problem is not necessarily an undersized main pipe. Restrictions are often created by local hoses, quick couplings, regulators, valves, dirty filters, sections installed “temporarily” during successive expansions, or a single bottleneck upstream of a large end use.
This is a typical case in which a new compressor would be a premature purchase. Additional capacity in the compressor room does not remove a local flow restriction – it may merely encourage operators to increase pressure further.
6. Air receivers and buffering short demand peaks
An air receiver acts as both storage and a stabilizer. It can reduce the effect of short demand spikes on compressor operation and network pressure. Its volume is not the only factor, however: location, the permissible pressure swing and connection capacity also matter.
For peak demand, three questions must be answered: how large is the additional flow, how long does it last, and what minimum pressure must be maintained? Only these data allow you to determine whether the issue can be solved with buffering or whether the demand lasts long enough to require additional source capacity.
DOE notes that short-duration high demand can be met from air stored in a receiver and that demand analysis should precede the addition of another compressor. In practice, a local receiver serving an intermittent high-demand end use may be more effective than increasing the capacity of the entire compressor room – provided the network can recharge it correctly between cycles.
7. Drying, filtration and the air quality actually required
Air treatment is needed to provide the parameters required by the process, not the “best possible” air quality throughout the plant. Excessive drying or filtration can increase energy costs through additional auxiliary demand and pressure drops.
ISO 8573-1 classifies compressed-air purity with respect to, among other things, particles, water and oil. This does not mean every end use requires the same class. The requirement should follow from the process, product, equipment or applicable quality specification.
For an energy assessment, it is useful to check:
- pressure dew point at the dryer outlet and – where necessary – in a critical part of the network;
- pressure drop across filters and dryers;
- condition of filter elements;
- dryer regeneration method and purge-air consumption;
- electrical energy used by the dryer, heaters, blowers or auxiliary equipment;
- system behaviour at part flow;
- actual quality requirements in individual zones.
DOE explicitly notes that drying below the required pressure dew point creates unnecessary cost. For the same reason, there is little justification for maintaining an expensive air-quality class throughout the entire network when only a small group of end uses has higher requirements that can be met locally.
8. Leaks – important, but not the only source of losses
Leaks should be located and repaired, but their significance should not be described using one universal percentage. In one plant they may be the dominant loss; in another, a much greater problem may result from controls, excessive pressure or unsuitable end uses.
Actual flow is the best basis for quantitative assessment. During non-production periods, when useful end uses have been properly isolated, baseline flow can help estimate the overall level of losses. Alternatively, methods based on compressor duty cycles or pressure-decay tests can be used, depending on system conditions. Leak locations are identified using acoustic or ultrasonic methods.
The cost of leakage should be calculated using the plant’s own system data. If leak flow Q and the system’s actual specific power SP are known and both refer to the same reference conditions, the approximate power required to supply that flow is P ≈ Q × SP. Annual energy can then be estimated as E ≈ P × h, where h is the actual time the system remains pressurized. This approach is more useful than converting all leaks using one percentage of production.
It is also necessary to check whether compressor controls will actually “capture” the energy benefit after repairs. If demand falls but several compressors continue to operate unloaded, the sequence or setpoints may need to be adjusted.
The detailed process of locating leaks should be treated as a separate diagnostic scope: compressed air leak detection.
9. End uses and artificial demand
The final place to look for the causes of high consumption is where the medium is used. Compressed air is sometimes used because it is readily available, not because it is the best energy source for a given task.
Check blow-offs, cooling, drying, cleaning, pneumatic conveying, vacuum generation, nozzles, open pipes, tools and end uses with removed or incorrectly set regulators. For each significant end use, the required pressure, flow, cycle time and the possibility of replacing compressed air with another technology should be considered.
Artificial demand is additional flow caused by maintaining a higher pressure than an end use actually requires. It applies particularly to unthrottled or poorly regulated applications and to leaks. Raising pressure throughout the network to “help” one machine can therefore increase consumption at many other points.
If a single end use requires higher pressure, consider a local solution – for example a modified connection, a suitable receiver, a separate pressure zone or a local booster – rather than increasing the parameter throughout the plant.
10. Only now: controls, compressor configuration and infrastructure
After the preceding stages, modernization options can be compared. Depending on the data, the solution may be to adjust pressure bands, change the sequence of several compressors, introduce master control, change the role of a variable-speed unit, enlarge or relocate a receiver, rebuild part of the piping, separate pressure zones, modernize treatment equipment, or change how an end use operates.
Only at this point should the question of a new compressor be raised. Purchase is justified when, after unnecessary demand has been reduced and the network checked, there is still a documented problem with capacity, efficiency, technical condition or the fit of the existing equipment to the operating profile.
If replacement is planned, comparing motor power alone is not enough. Relevant factors include capacity at the required pressure, total package power, unloaded power, part-load characteristics and the role of the unit within the entire compressor room. CAGI data illustrate this difference through “power per flow” and specific power values referenced to a defined pressure.
11. Heat recovery as a separate, additional benefit
Heat recovery is worth analysing, but it should not replace demand optimization. If a compressor produces unnecessary air, making use of the resulting heat does not make that air generation energetically justified.
First reduce unnecessary compressed-air consumption, stabilize source operation and determine actual loaded hours. Only then can the available heat be calculated and matched to a heat sink. DOE identifies typical uses including space heating, process heating and water heating. The actual benefit, however, depends on compressor cooling type, temperatures, simultaneous operation of the source and heat sink, seasonality and the efficiency of the heat source being displaced.
In practice, check:
- how many hours the compressor actually operates under load;
- what temperature and thermal power are available;
- whether a stable heat demand exists at the same time;
- how long and costly the transmission route is;
- whether heat exchangers, pumps, fans and additional controls are required;
- what energy carrier or fuel the recovered heat will actually displace.
The broader topic is described on our heat recovery page.
What measurements are needed to assess a compressed air system?
Good measurements should be time-synchronized. A power chart without flow says little, just as flow without information about pressure and production status does. The greatest value comes from aligning the parameters on one time axis.
| Measurement or data | Where / how to measure | What it allows you to assess |
|---|---|---|
| Electrical power and energy | separately for compressors or at a common supply point; include significant auxiliary equipment within the system boundary | actual energy cost, unloaded operation, effect of controls |
| Flow | main header and, where necessary, zones, selected compressors and critical end uses | demand profile, peaks, non-production flow, zone balance |
| Pressure | compressor-room outlet, before/after treatment, main header, remote points and critical end uses | pressure level and stability, dynamic drops, local restrictions |
| Pressure dew point | downstream of the dryer and – where required – in a critical zone | whether drying is matched to process requirements |
| Compressor operating states | controller logs or parallel logging of power and signals | load/unload, shutdown, VSD, number of starts, interaction of multiple units |
| Operating hours | controllers, master system, meters | equipment utilization, maintenance planning, share of unproductive operation |
| Production data | ERP/MES/SCADA, shift reports or other reliable plant data | normalization of energy and flow to production output |
| End-use requirements | documentation, local measurement, cycle observation | minimum required pressure, flow and quality |
| Dryer and filter data | pressure drops, auxiliary energy, regeneration method, element condition | treatment cost and its effect on the entire system |
| Leaks | detection + flow measurement during controlled periods | location and quantitative assessment of losses |
The measurement period should be representative, not automatically the same length every time. A plant with a stable profile requires a different period from a site operating three shifts, weekends, multiple products and frequent changeovers. If shutdowns are important, they must be included in the logging period. If the process is seasonal, a one-week measurement may not be sufficient for an annual assessment without additional historical data.
Why is specific energy consumption more important than nameplate power?
Nameplate power primarily indicates drive size. It does not show how much air the unit delivers under actual conditions, how it performs at part load, or how much energy the entire system consumes as demand changes.
For a compressor or an entire compressor room, an indicator that relates power draw to flow is more useful. In its simplest form:
SP = P / Q
where P is the actual system input power and Q is the delivered flow at clearly defined reference conditions. In SI units, for example, kW/(m³/min) can be used. For a billing period, E/V can be calculated analogously, i.e. kWh per specified volume of compressed air. Flow reference conditions must be documented because values stated in m³, Nm³ or other referenced units are not comparable without a definition.
Simple example: two compressors operate at comparable pressure. The first draws 70 kW and delivers 10 m³/min, giving 7.0 kW/(m³/min). The second draws only 60 kW but delivers 7.5 m³/min, giving 8.0 kW/(m³/min). In this case, lower instantaneous power does not mean better specific efficiency.
In a system with several compressors, a system-level specific power indicator is even more useful: the sum of the actual power of the operating units divided by the total measured flow. This immediately reveals the effect of sequencing, unloaded operation and inefficient interaction between multiple compressors.
DOE also recommends correlating energy and flow with production. If production rises after a process change, total kWh may increase despite improved efficiency. In addition to SP, it is therefore useful to monitor indicators such as compressor-room kWh per tonne or unit of product and m³ of compressed air per unit of production.
When is buying a new compressor premature?
A new compressor can solve a source-side problem, but only when the source is the actual cause of the limitation. It will not automatically solve problems in the network, controls or end use. Before investing, at least the situations below should be ruled out.
| Symptom | Premature conclusion | What to check first |
|---|---|---|
| Low pressure only at the far end of the plant | “the compressor is too small” | simultaneous pressure in the compressor room and at the machine, pressure drops across filters, hoses, valves and the connection |
| A short flow peak starts an additional compressor | “we need more capacity” | peak duration, receiver capacity, local buffering and control settings |
| Two compressors frequently run unloaded | “we need a new VSD” | start sequence, overlapping pressure bands, trim capacity and storage volume |
| One machine requires higher pressure | “increase pressure throughout the plant” | local booster, separate zone, connection modification or selection of a different end-use solution |
| The compressor room shows high flow at weekends | “we are missing a modern compressor” | leaks, valves left open, blow-offs, unnecessary end uses, automatic drains |
| Pressure downstream of treatment is clearly lower | “the compressor cannot maintain its parameters” | pressure drop across the dryer, filters, separators, valves and fittings |
| Energy consumption rises with production | “the compressor has lost efficiency” | kWh and flow per unit of production, pressure, load profile and process changes |
A useful external example is the Darigold project described by the DOE Better Plants program. The plant maintained high pressure in the compressor room, yet remote end uses still experienced large fluctuations. The analysis identified distribution restrictions; piping modifications stabilized pressure and only then made it possible to reduce the pressure level. This illustrates why a problem at the end of the network should not automatically be addressed with a larger compressor or a higher setpoint.
How should the effect of actions be assessed without fixed savings percentages?
The effect should be assessed by comparing a measurable baseline with the post-change condition under production conditions that are as comparable as reasonably possible. The calculation method depends on the type of action.
Pressure reduction: before the change, the minimum requirements of end uses, dynamic pressure drops, flow and compressor characteristics must be known. After the change, power, energy, flow, pressure and specific indicators are compared. A fixed saving per bar should not be assumed in advance.
Leak repair: the basis is measured or reliably estimated loss flow, the system’s actual SP and the time for which the installation remains pressurized. After repairs, check whether the number of operating compressors, loaded time or power draw has decreased.
Control changes: compare primarily the power profile, load/unload states, number of starts, pressure and flow. The benefit should result from better matching generation to actual demand.
Compressor replacement: the comparison should include not only the efficiency of the new unit at its rated point, but also the expected part-load profile and interaction with the remaining machines. Replacing equipment without addressing the cause of excessive demand may deliver a much smaller benefit than a catalogue comparison would suggest.
How should the implementation sequence be determined?
The diagnostic sequence and the investment sequence are not always identical. After measurements, it is useful to build an action list based on dependencies: what removes the cause, what requires an earlier change, and what can be implemented independently.
Usually, actions that do not constrain later decisions are implemented first: correcting incorrect settings, organizing control logic, repairing confirmed leaks and eliminating clearly unnecessary end uses. The next step can address infrastructure – pressure drops, local storage, treatment and separation of zones. Compressor purchase or replacement should be based on the profile after unnecessary demand has been reduced, so that new equipment is not sized for losses that can be eliminated.
For larger changes, it is good practice to implement them in stages and keep monitoring in place. If flow decreases after leak repair but power does not, this indicates that the controls should be adjusted. If a network modification reduces dynamic pressure losses, source setpoints can be reassessed. One action often creates the opportunity for the next.
Which indicators should be monitored after optimization?
After changes have been implemented, comparing a single energy bill is not enough. It is useful to maintain a small set of straightforward indicators:
- total compressor-room kWh;
- average and maximum flow;
- system specific power (SP) at a defined pressure;
- compressor-room kWh per unit of production;
- m³ of compressed air per unit of production;
- minimum and maximum pressure at critical points;
- pressure drop across treatment equipment and main network sections;
- share of loaded and unloaded hours for individual compressors;
- non-production flow;
- pressure dew point, where it is a critical process parameter.
The data do not need to come from an extensive monitoring system from day one. What matters most is maintaining a consistent measurement boundary and comparable conditions. In systems with significant energy consumption, continuous monitoring of system and energy parameters is worth considering so that deterioration becomes visible before it translates into several months of higher costs.
What should a plant do as the first step?
If it is not clear where the losses occur, I would not start with a compressor catalogue. First, I would compile a list of sources and end uses, controller data, the production schedule and information about pressure and air-quality problems. Then energy, flow and pressure should be logged simultaneously over a period covering both typical and atypical operating states.
On this basis, a balance can be developed: how much air is generated, how much energy it costs, where pressure is lost, what share of the flow performs useful work, and which equipment dictates the parameters of the entire installation. Only then can improvement measures be put in the right order.
If such an analysis is required for a specific plant, a compressed air system audit can combine operating data and measurements into recommendations for the source, treatment, network and end uses. If the problem has already been narrowed down exclusively to leakage, a separate leak-detection survey may be sufficient. To select the appropriate scope, contact Energy Trend.
Frequently asked questions
Do compressed air system measurements always have to last a week?
No. The measurement period should cover representative operating modes. It can be shorter in a plant with stable production, while shift-based, weekend, seasonal or highly variable production may require longer datasets or a combination of short-term measurements and historical data from plant systems.
Will a variable-speed compressor always reduce energy consumption?
No. Speed control is particularly useful when a unit is intended to cover an appropriate range of variable demand. If the profile is mainly constant, or if the variable-speed compressor is poorly integrated into the sequence of several compressors, the result may be far from optimal. The decision should be based on the flow profile and the characteristics of all sources.
Is ISO 11011 mandatory for every company?
The technical standard itself does not create a generally applicable legal obligation to perform an assessment in accordance with ISO 11011. It is, however, a recognized reference for the system-level assessment of compressed-air energy efficiency and may be required by a contract, specification or an organization’s internal standard.
Should heat recovery be the first compressor-room modernization measure?
There is no universal rule of this kind. First, unnecessary compressed-air generation should be reduced and the actual operating profile established. Heat recovery can then be analysed as an additional opportunity to replace another heat source, provided a suitable heat sink exists and the timing of supply and demand is compatible.
Sources
- ISO 11011:2013 – Compressed air — Energy efficiency — Assessment and ISO information on the start of work on Edition 2 in 2026: ISO/AWI 11011.
- ISO 8573-1:2010 – Compressed air — Part 1: Contaminants and purity classes and the project for the next edition: ISO/AWI 8573-1.
- U.S. Department of Energy, Improving Compressed Air System Performance: A Sourcebook for Industry, Third Edition.
- Better Buildings & Better Plants, Compressed Air and the case study Darigold: Compressed Air System Optimization.
- Compressed Air & Gas Institute, Air Compressor Performance Verification and Testing Results.